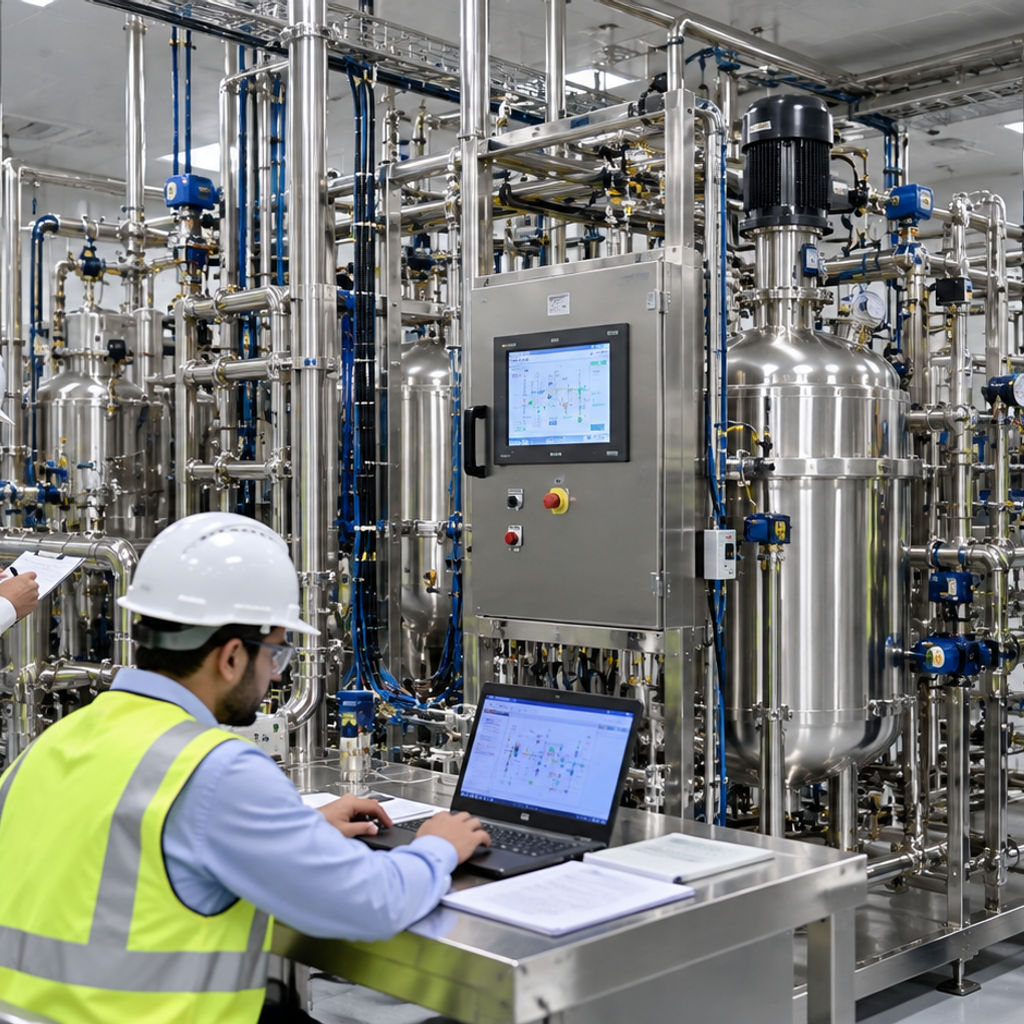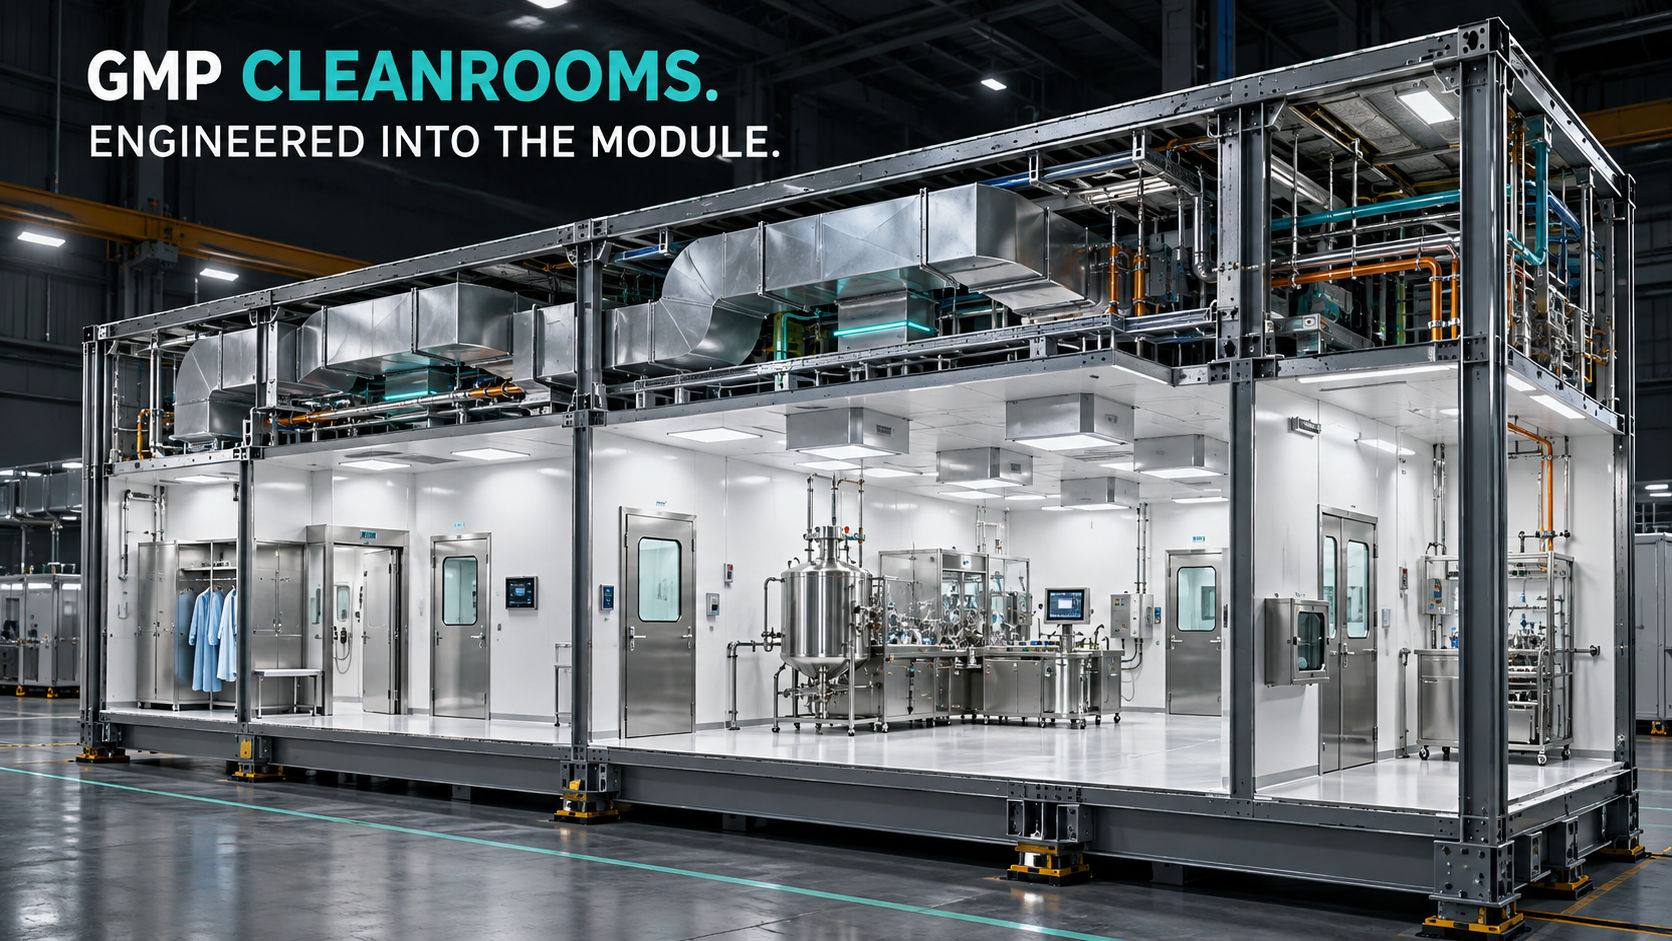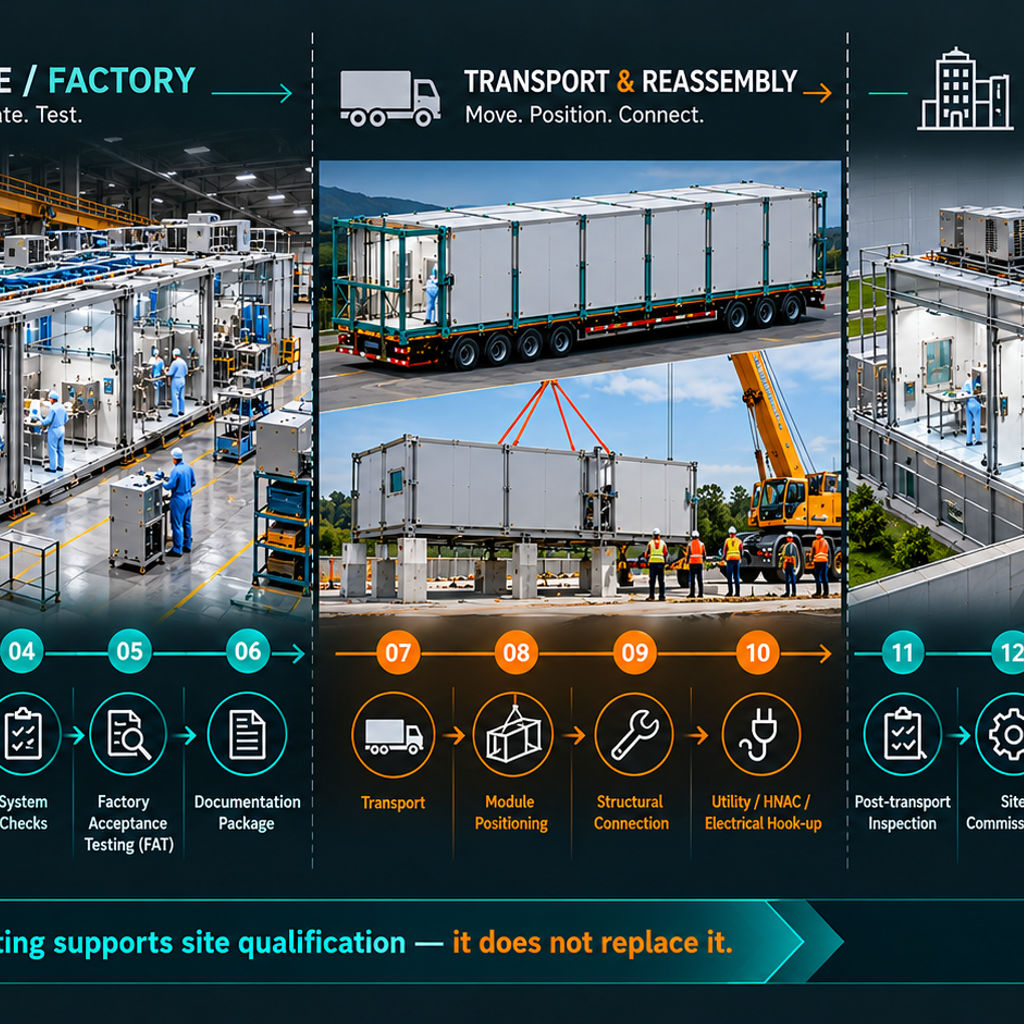
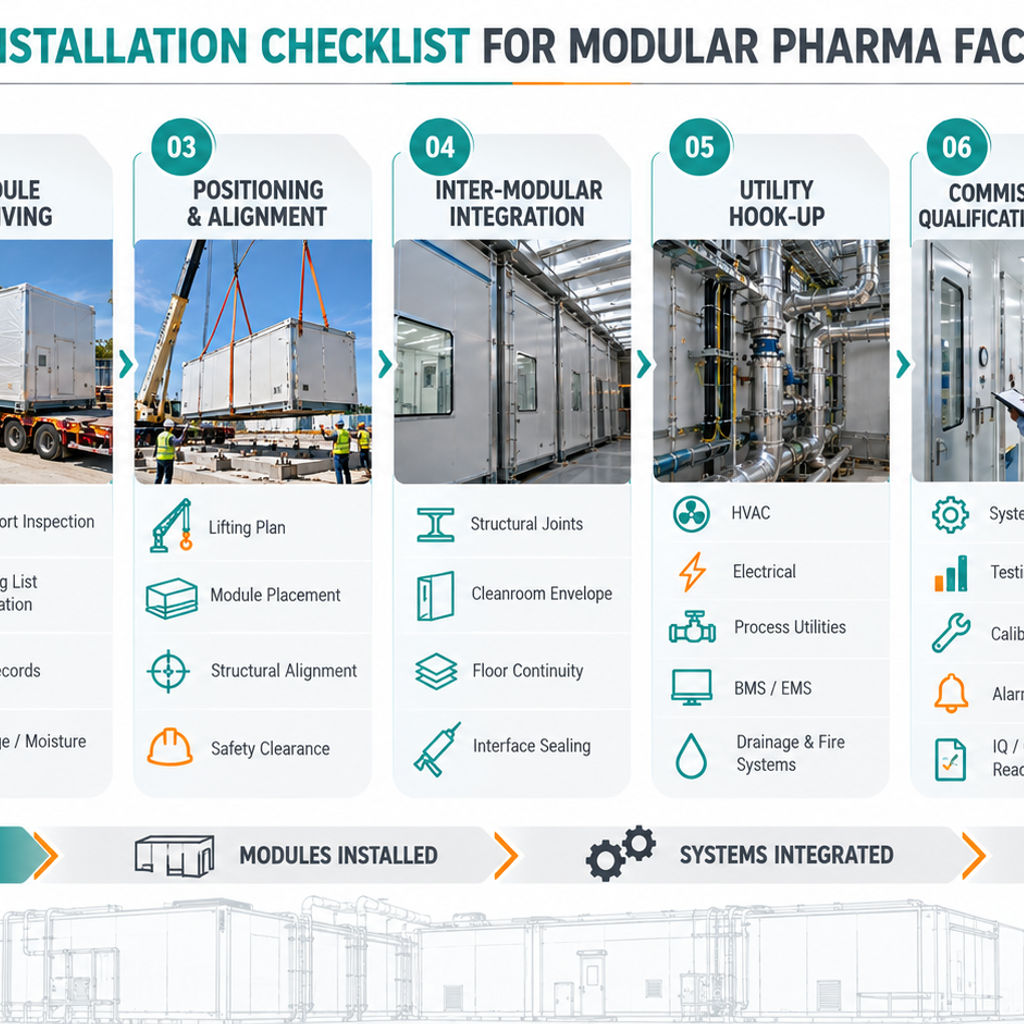
Site Installation Checklist for Modular Pharma Facilities

In modular pharmaceutical projects, installation is the stage where design, logistics, GMP requirements, utilities, cleanroom performance, and documentation come together on site. Since a major part of the facility is already engineered, manufactured, and tested off site, the site must be fully prepared before the modules arrive.

For pharmaceutical manufacturers, CDMOs, biotech companies, vaccine manufacturers, and API facilities, a modular approach can support faster project delivery and better control over construction quality. However, the final success depends on how smoothly the facility is received, positioned, connected, commissioned, and validated.

A clear site installation checklist helps reduce delays, avoid rework, maintain GMP design intent, and create a structured path from module placement to operational readiness.

Why Site Readiness Matters

A modular pharmaceutical facility cannot be treated like a standard construction package. By the time modules reach the project site, the civil base, utility connections, unloading area, crane access, safety clearances, and installation sequence should already be confirmed.

If the foundation level is incorrect, utility points do not match, or access for lifting is restricted, the installation timeline can be affected. For GMP facilities, these issues can also impact cleanroom performance, personnel flow, material flow, and commissioning readiness.

This is why Design & Engineering should define site interfaces, utility loads, module placement, HVAC requirements, and installation logic before off-site fabrication begins.
Civil and Structural Readiness

Before the modules arrive, the site team should verify that the civil and structural work is ready to receive the facility. This includes checking foundation levels, load-bearing capacity, anchor points, drainage, access roads, lifting radius, and temporary staging areas.

The module base must match the approved layout and structural design. Any mismatch at this stage may create alignment issues during placement or inter-modular connection.

Key checks include: 

  • Foundation readiness and level verification 
  • Structural support alignment 
  • Load-bearing confirmation 
  • Crane access and lifting radius 
  • Module unloading area 
  • Temporary staging area 
  • Drainage and waterlogging control 
  • Access for installation teams and equipment 
  • Site safety barricading 

Module Receiving and Logistics

The receiving stage is critical because modular pharma facilities are transported as pre-engineered units. Each module must be protected from physical damage, moisture, dust, and contamination risk during transport, unloading, and positioning.

Before shipment reaches the site, the project team should confirm transport route clearance, crane availability, lifting permits, unloading sequence, and temporary storage requirements. After delivery, modules should be inspected against packing lists, drawings, and FAT records.

This connects directly with Off-site Modular Construction, where modules are built under controlled conditions before being transported to the final location.

Cleanroom and Layout Integrity

A modular facility must maintain the approved GMP layout after installation. Personnel flow, material flow, gowning sequence, airlock position, process movement, waste movement, and maintenance access should remain aligned with the original facility design.

For modular cleanrooms, sterile areas, biotech suites, or API facilities, this is especially important. Room positioning, door direction, pass box placement, cleanroom panel joints, wall and floor interfaces, and classified area segregation must be verified during installation.

Strong Pharmaceutical Facility Design and Cleanroom Engineering ensure that the facility is designed around the product, process, and GMP requirements from the beginning.

Utility Integration and Hook-up

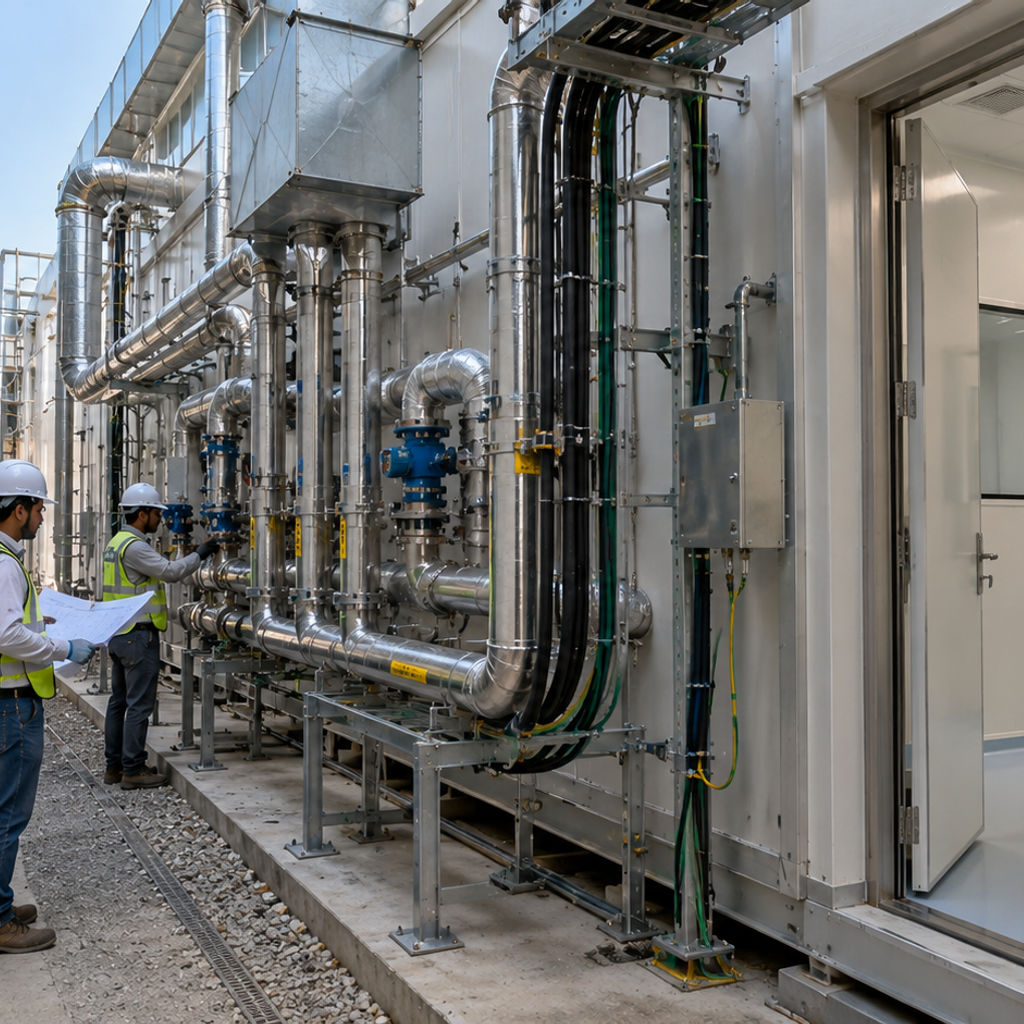
Utility integration is one of the most important parts of modular pharma facility installation. Modules may arrive with pre-installed HVAC, electrical systems, process piping, cleanroom panels, EMS, BMS, and other services. These systems still need to be connected correctly to site infrastructure.

The checklist should cover electrical connections, HVAC ducting, compressed air, chilled water, process utilities, drainage, instrumentation, control cabling, fire safety interfaces, earthing, leak testing, and pressure testing.

For a GMP manufacturing facility, utility performance directly affects product quality. HVAC, HEPA filtration, temperature, humidity, pressure cascades, and environmental monitoring must be verified before commissioning.

This is where Installation & Hook-up becomes a GMP-critical activity, not just a construction step.
Inter-Modular Connections

When multiple modules are joined together, the interfaces between them are as important as the modules themselves. Structural joints, cleanroom envelope sealing, flooring continuity, HVAC ducts, utility piping, electrical cabling, and monitoring systems must connect without compromising the facility design.

For modular cleanrooms, even small gaps or poorly finished joints can affect pressure control, cleanability, and contamination control. Inter-modular connection should therefore be planned, inspected, and documented carefully.

FAT and Site Verification

Factory Acceptance Testing helps verify equipment, systems, controls, and module integration before shipment. It allows many technical issues to be corrected in the factory environment instead of at the project site.

However, FAT does not replace site verification. After transportation and installation, the team must confirm that modules, utilities, instruments, controls, alarms, HVAC systems, and safety systems are still performing as intended.

FAT records, open points, inspection reports, and site verification documents should be available before commissioning begins.

Commissioning and Validation Readiness

Commissioning confirms that installed systems are connected, energized, tested, and ready for qualification. This includes HVAC start-up, utility checks, pressure balancing, filter installation, control system communication, alarm testing, and safety system verification.

After commissioning, the facility moves toward qualification and validation. IQ, OQ, and PQ documentation should be supported by approved drawings, calibration records, material certificates, FAT reports, commissioning records, change controls, and SOP readiness.

Any change made during installation should be reviewed through proper change control, especially if it affects room classification, pressure cascade, utility routing, monitoring systems, personnel flow, or material flow.

This makes Validation & Commissioning an essential part of the installation journey.

Documentation and Handover

Installation is not complete without proper documentation. Missing drawings, incomplete FAT closure, open punch points, or unresolved deviations can delay commissioning and validation.

The final handover package should include approved drawings, as-built drawings, installation records, utility test reports, FAT documents, commissioning reports, calibration certificates, material certificates, change control records, deviation closure, training records, and final handover documentation.

For pharmaceutical manufacturers, documentation supports GMP compliance, maintenance, inspection readiness, and future expansion.

Why Choose Modular Mobile Facility (MMF)?

Modular Mobile Facility supports pharmaceutical companies through an integrated delivery model covering Design & Engineering, Off-site Modular Construction, Manufacturing, Factory Acceptance Testing, Transportation, On-Site Installation, Installation & Hook-up, Validation Support, and Commissioning.

MMF’s approach is built around controlled off-site construction, GMP-focused engineering, faster project delivery, and structured on-site installation. By moving a significant part of facility construction and testing into a controlled workshop environment, MMF helps reduce site dependency and supports a smoother path from design to operational readiness.

For pharmaceutical manufacturers, biotech companies, CDMOs, vaccine facilities, and API producers, MMF provides turnkey modular solutions engineered for compliant and efficient pharmaceutical manufacturing.

Frequently Asked Questions

1. What is a site installation checklist for modular pharma facilities?

A site installation checklist for modular pharma facilities is a structured readiness document used before, during, and after module installation. It covers civil readiness, module receiving, lifting, placement, utility hook-up, cleanroom interfaces, HVAC integration, commissioning, documentation, and validation readiness. It helps pharmaceutical project teams reduce rework, maintain GMP design intent, and move smoothly from installation to qualification.

2. Why is site readiness important for a modular pharmaceutical facility?

Site readiness is critical because modular facilities arrive with many systems already fabricated and integrated. If foundations, utilities, access routes, lifting areas, or connection points are not ready, installation delays can occur. For GMP facilities, poor site readiness can also affect cleanroom performance, material flow, personnel flow, utility integration, and commissioning timelines.

3. What should be checked before modular pharma modules arrive on site?

Before modules arrive, teams should check foundation levels, structural supports, crane access, unloading areas, temporary storage, utility stub-outs, safety clearances, installation drawings, and site permits. The project team should also confirm module arrival sequence, lifting plans, manpower readiness, and documentation availability to ensure smooth installation.

4. How does FAT support modular pharma facility installation?

Factory Acceptance Testing helps verify equipment, systems, and module integration before shipment. It allows issues to be identified and corrected in the factory environment rather than at the project site. In modular pharma facilities, FAT can reduce site installation risk, shorten commissioning time, and provide documentation support for later qualification activities.

5. Do modular cleanrooms require validation after installation?

Yes. Modular cleanrooms still require qualification and validation after installation. Even if the cleanroom is pre-fabricated and tested off site, final verification must confirm that the installed facility meets approved design and GMP requirements. This may include IQ, OQ, PQ, airflow testing, pressure cascade verification, HEPA filter integrity testing, and environmental monitoring checks.

6. What utilities are important during modular pharma facility hook-up?

Important utilities include HVAC, electrical power, compressed air, process utilities, water systems where applicable, drainage, BMS, EMS, fire safety systems, instrumentation, and control wiring. These utilities must be correctly connected, tested, and documented before commissioning and qualification can proceed.

7. What is the difference between installation and commissioning in modular pharma projects?

Installation focuses on placing modules, connecting structures, completing utility hook-ups, and ensuring physical readiness. Commissioning confirms that systems are installed correctly and operate as intended. In pharmaceutical projects, commissioning prepares the facility for qualification and validation activities such as IQ, OQ, and PQ.

8. How can MMF help with modular pharma facility installation?

MMF supports modular pharma facility projects through design, engineering, off-site manufacturing, FAT, transportation, on-site installation, hook-up, commissioning, and validation support. This integrated approach helps pharmaceutical companies reduce site complexity, maintain GMP alignment, and achieve a more controlled path to operational readiness.
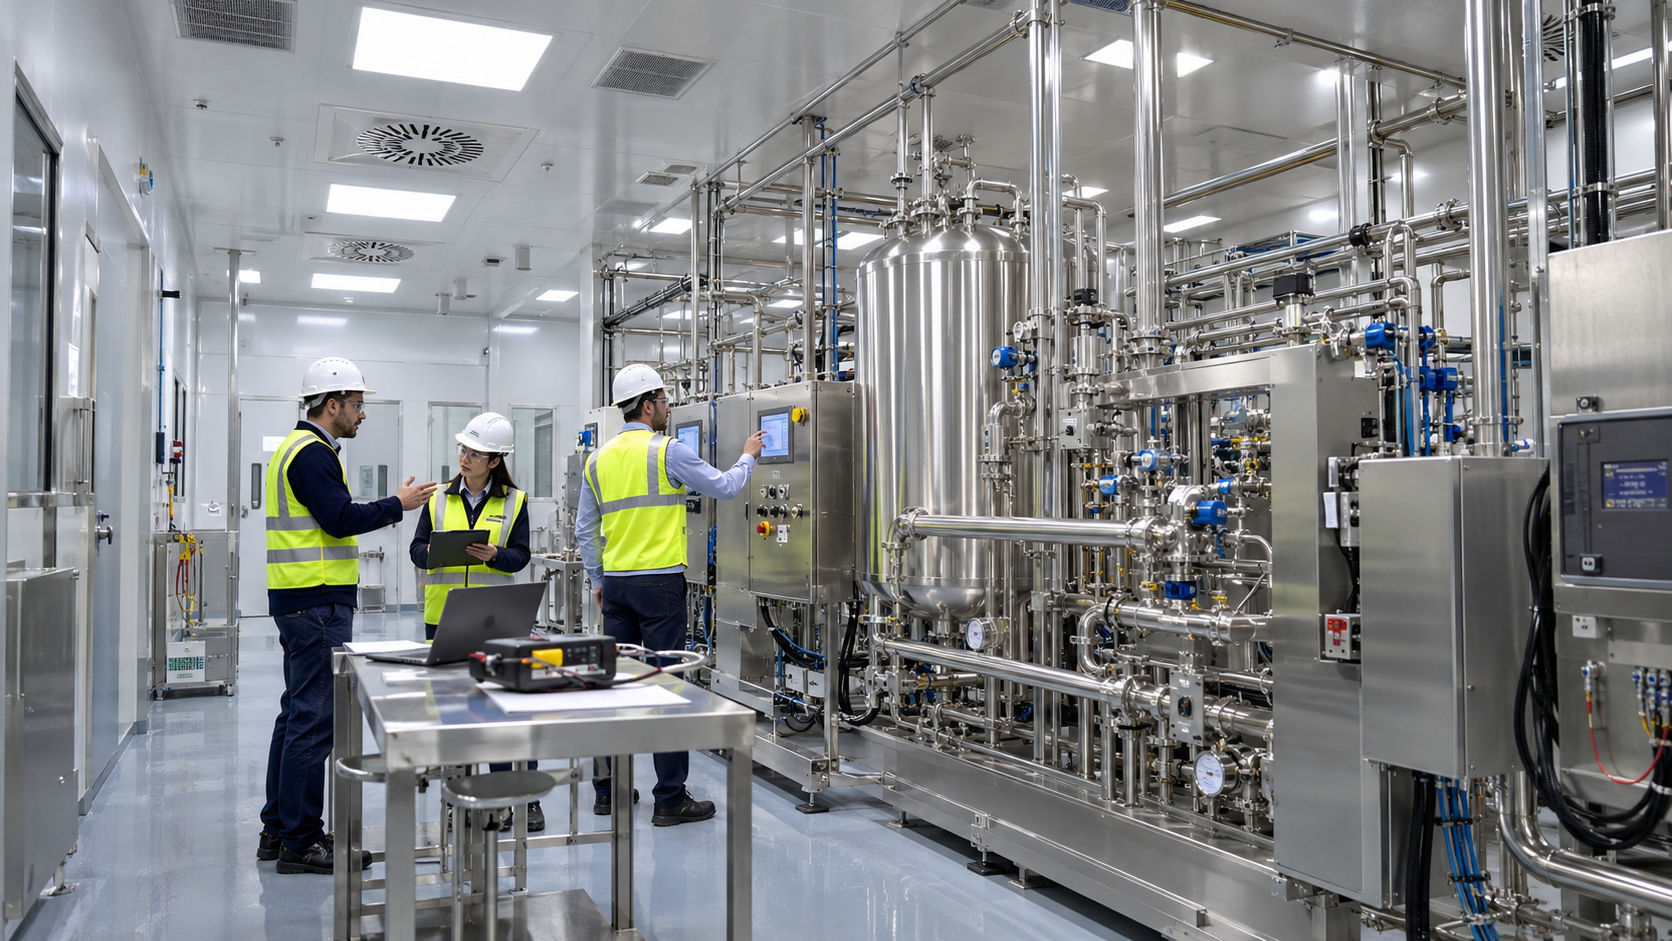
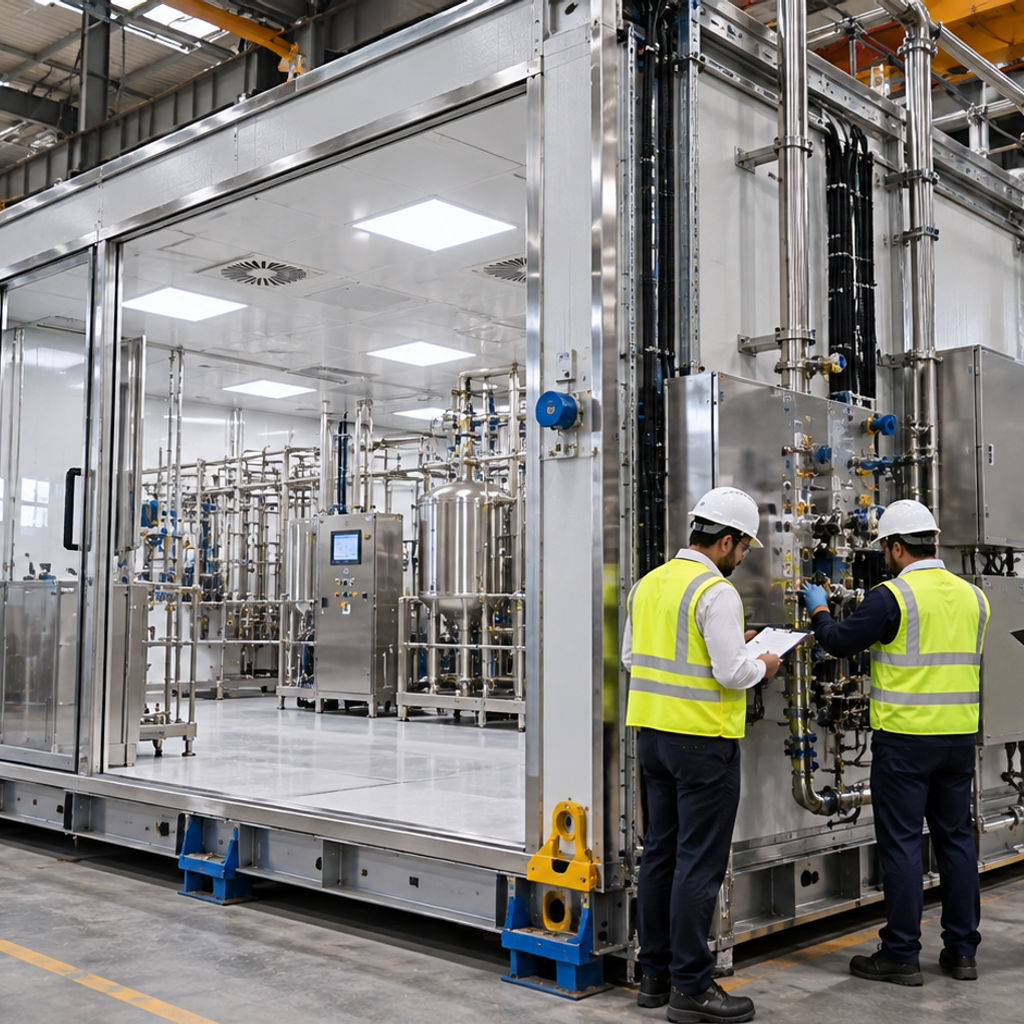
How FAT Reduces Risk in Modular Pharma Projects

In modular pharma projects, the costliest risks often appear after the module reaches the site. A missed utility interface, an unverified control sequence, an access limitation, or a pressure cascade issue can delay commissioning and affect GMP readiness. 

In conventional project delivery, many of these issues appear during site commissioning, when access is limited, timelines are compressed, and multiple contractors are working in parallel. In modular pharma projects, Factory Acceptance Testing in Modular Pharma Projects, shifts this risk forward. It allows critical systems to be checked in a controlled manufacturing environment before shipment and installation.

For pharmaceutical manufacturers, biotechnology companies, CDMOs, vaccine manufacturers, and API producers, FAT is not only a testing activity. It is a project risk-reduction tool. When planned correctly, FAT helps verify whether the modular pharmaceutical facility is aligned with user requirements, GMP intent, design specifications, and operational expectations before it reaches the site.

Why FAT Matters in Modular Pharma Facilities

A modular pharmaceutical facility is not simply a prefabricated structure. It is an integrated manufacturing environment that may include cleanrooms, HVAC systems, HEPA filtration, pressure cascades, process utilities, electrical systems, automation, EMS, BMS, and process equipment. The value of modular execution lies in bringing many of these elements together off-site, under controlled conditions.

This is where Design & Engineering plays a critical role. FAT becomes effective only when the project has a clear design basis, defined user requirements, approved drawings, utility loads, equipment layouts, and operating philosophy. Without this foundation, FAT becomes a checklist exercise. With proper engineering, it becomes a structured verification process.

In modular projects, the facility is assembled and tested before shipment. This makes it possible to identify design gaps, interface issues, equipment access concerns, utility mismatches, and control-sequence errors earlier in the project lifecycle. Correcting these issues at the module construction facility is usually more practical than resolving them after delivery, placement, and site hook-up.

FAT as a Risk-Control Step Before Shipment

Factory Acceptance Testing reduces risk by confirming that the module or equipment package has been built according to approved specifications. It helps project teams verify whether the delivered system matches the URS, design documents, P&IDs, equipment specifications, layout drawings, utility requirements, and automation logic.

For a modular manufacturing facility, this may include checks related to equipment installation, cleanroom finishes, utility routing, access panels, instrumentation, alarm logic, control panels, room zoning, pressure cascade logic, and hook-up readiness. The objective is not to complete final qualification at the factory. The objective is to reduce uncertainty before the module is transported.

This is especially important because modular pharma projects involve multiple interfaces. A process skid may depend on clean utilities. The cleanroom may depend on HVAC balancing. HVAC performance may depend on ducting, filters, sensors, dampers, and controls. Automation may depend on field instruments, alarms, interlocks, and communication with BMS or EMS.

Through Off-site Modular Construction, many of these systems can be brought together before site work reaches its most critical stage. FAT allows project teams to verify whether these systems are coordinated, accessible, and ready for shipment.

Reducing Design and Engineering Risk

One of the most important benefits of FAT is its ability to reveal design and coordination issues before they become site-level delays. Even with detailed engineering, modular projects can face practical challenges once equipment, utilities, cleanroom panels, HVAC ducts, and controls come together in the same physical space.

FAT helps confirm whether equipment is positioned correctly, whether maintenance access is available, whether instruments are reachable, whether utility routes are practical, and whether the module can support the intended operating and cleaning requirements. These are not minor details in pharmaceutical manufacturing. They directly affect GMP readiness, operational efficiency, and long-term maintainability.

For example, a pressure sensor may be technically specified but poorly located. A utility connection may be correctly sized but difficult to access after installation. A control panel may be functional but positioned in a way that complicates operation. FAT gives the project team an opportunity to identify and resolve these issues while the module is still in a controlled workshop environment.

This reinforces the importance of Pharmaceutical Facility Design as an early-stage risk management activity. A well-designed facility makes FAT more meaningful, and a well-executed FAT validates the practical readiness of that design.

Managing GMP and Cleanroom Risks

In GMP manufacturing facilities, facility performance is closely linked to contamination control, personnel flow, material flow, environmental control, and utility reliability. FAT helps project teams review whether the modular cleanroom and its supporting systems are aligned with the intended GMP strategy.

For modular cleanrooms, this may involve checking room finishes, panel joints, door interlocks, return air paths, pressure cascade logic, HVAC integration, HEPA filter installation readiness, EMS points, BMS connections, and alarm conditions. While final cleanroom qualification must be completed after installation, pre-shipment checks help reduce the risk of discovering major gaps during commissioning.

FAT also supports better documentation discipline. When observations, deviations, corrective actions, and acceptance criteria are documented before shipment, the project team has clearer evidence of what was verified at the factory and what must be reconfirmed at the site.

This is where Validation & FAT becomes an important part of integrated project delivery. FAT should be connected with later qualification, commissioning, and validation support. It should not be treated as a separate event disconnected from site readiness.

What Dual FAT Means in MMF Projects

For modular pharma projects, a dual FAT approach can further reduce risk. Dual FAT is not a separate regulatory term, but it is a practical engineering approach that fits modular execution well.

The first FAT is typically performed at the OEM or vendor level. This may apply to critical process equipment, clean utility skids, HVAC packages, automation panels, or other engineered systems. At this stage, the focus is on verifying whether the individual package performs according to its specification.

The second FAT is performed after these systems are integrated into the modular facility. This is where the focus shifts from equipment readiness to facility readiness. The question is no longer only whether a skid works. The question is whether the skid, cleanroom, utilities, HVAC, automation, and module interfaces work together as an integrated pharmaceutical manufacturing environment.

For MMF projects, this dual FAT approach is highly relevant because the facility is engineered, constructed, assembled, and checked off-site before transportation. It allows critical systems to be verified first as independent packages and then again as part of the modular facility.

This supports a clearer transition from Manufacturing to Factory Acceptance Testing, and then from FAT to Installation & Hook-up at the project site.

FAT Does Not Replace SAT, Commissioning, or Validation

FAT reduces risk, but it does not eliminate the need for Site Acceptance Testing, commissioning, or validation. This distinction is important for pharmaceutical decision-makers.

Some checks can be meaningfully completed before shipment. Others must be repeated or confirmed after transportation, unloading, placement, inter-modular connections, utility hook-up, and final site conditions. For example, a control sequence may be verified during FAT, but site power, final utility connections, pressure balancing, airflow verification, and cleanroom qualification must be confirmed after installation.

A strong FAT strategy clearly defines what is accepted at the factory, what is carried forward to site testing, and what must be confirmed during commissioning and validation. This prevents overclaiming and helps maintain compliance integrity.

Through On-Site Installation, the modular facility moves from factory-tested readiness to site-specific readiness. Placement, inter-modular connections, hook-up, commissioning, and validation support are essential to confirm that the module performs as intended in its final operating environment.

What a Strong Modular FAT Protocol Should Include

A FAT protocol for modular pharma projects should be built around risk, not only around inspection. It should reflect the URS, approved drawings, design specifications, GMP requirements, equipment data, automation logic, and operating philosophy.

A strong protocol may include verification of construction completion, equipment installation, utility routing, instrument tagging, access for operation and maintenance, automation sequences, alarms, interlocks, cleanroom finishes, HVAC integration, pressure cascade logic, EMS/BMS points, and hook-up readiness.

It should also clearly identify acceptance criteria. This helps avoid subjective decisions during FAT. Each test should define what is being verified, how it will be checked, what documentation is required, and what action is needed if the result is not acceptable.

For modular projects, the FAT protocol should also define what may be affected by transportation. Any function that could change during shipment, lifting, placement, or site reconnection should be reconfirmed during SAT, commissioning, or validation.

How FAT Supports Faster Project Delivery

One of the reasons pharmaceutical companies consider modular pharma facilities is faster project delivery. However, speed is useful only when it is supported by control. FAT helps protect the schedule by reducing late-stage rework and improving visibility before shipment.

When issues are identified during FAT, they can be corrected while the module is still accessible and before the project depends on site availability. This reduces the likelihood of delays during installation and commissioning. It also improves coordination between engineering teams, vendors, validation teams, and site project managers.

For facility owners and investors, FAT improves confidence. It provides a structured view of project readiness before the facility leaves the factory. For plant heads and operations leaders, it helps confirm that the facility has been reviewed from an operational perspective before arriving at site.

This makes FAT a practical bridge between Off-site Modular Construction and Validation & Commissioning.

Why Choose Modular Mobile Facility (MMF)?

Modular Mobile Facility supports pharmaceutical companies with turnkey modular solutions designed for GMP compliance, faster project delivery, and scalable pharmaceutical infrastructure. MMF integrates Design & Engineering, Off-site Modular Construction, Factory Acceptance Testing, Transportation, Installation & Hook-up, Validation Support, and Commissioning into a connected project delivery model.

Because MMF manages modular facility delivery from design and engineering to FAT, transportation, installation, hook-up, validation support, and commissioning, FAT is not treated as a separate inspection event. It becomes part of the complete project-readiness strategy. 

For modular pharma projects, this integrated approach matters. FAT is most effective when it is planned from the beginning, aligned with design intent, connected with site installation, and supported through commissioning and validation. MMF’s approach helps reduce uncertainty by verifying key systems in a controlled environment before shipment and supporting the facility through final site readiness.

For pharmaceutical manufacturers, biotech companies, CDMOs, vaccine producers, and API manufacturers, MMF provides modular pharmaceutical facilities engineered around compliance, integration, and practical execution.

Frequently Asked Questions

1. What is FAT in a modular pharma project?

Factory Acceptance Testing is a pre-shipment verification process carried out before a modular facility, equipment package, or integrated system is transported to the site. In modular pharma projects, FAT helps confirm that the facility or system is built according to approved specifications, user requirements, and GMP design intent. It reduces the risk of discovering major issues during installation, commissioning, or validation.

2. Why is FAT important for modular pharmaceutical facilities?

FAT is important because modular pharmaceutical facilities combine cleanrooms, HVAC, utilities, equipment, controls, and automation within a factory-built environment. Testing these systems before shipment helps identify design gaps, interface issues, access concerns, and control-sequence problems early. This reduces site rework, protects the project schedule, and supports smoother commissioning.

3. What is dual FAT in modular pharma projects?

Dual FAT refers to a practical two-stage testing approach. The first FAT is performed at the OEM or vendor level for critical equipment or utility packages. The second FAT is performed after those systems are integrated into the modular facility. This helps verify both individual equipment readiness and overall facility integration before shipment.

4. Does FAT replace SAT in pharmaceutical projects?

No, FAT does not replace Site Acceptance Testing. FAT verifies systems before shipment, while SAT confirms performance after delivery, placement, hook-up, and site installation. In modular projects, some checks completed during FAT may remain valid, but functions affected by transportation, lifting, reconnection, or final site conditions must be reconfirmed onsite.

5. What should be checked during FAT for a GMP modular facility?

A FAT protocol for a GMP modular facility may include checks for construction completion, equipment installation, cleanroom finishes, utility routing, HVAC integration, pressure cascade logic, instrumentation, alarms, interlocks, EMS/BMS points, access for operation and maintenance, and hook-up readiness. The protocol should be based on URS, design documents, and risk assessment.

6. How does FAT reduce commissioning risk?

FAT reduces commissioning risk by identifying and resolving issues before the module reaches the site. Since systems are more accessible at the factory, corrections can be made earlier and with less disruption. This reduces late-stage troubleshooting, improves documentation readiness, and allows commissioning teams to focus on site-specific verification rather than unresolved factory issues.

7. Is FAT required for every modular pharma facility?

FAT is strongly recommended for modular pharma facilities, especially when the project includes complex equipment, cleanrooms, HVAC systems, process utilities, automation, or GMP-critical interfaces. The exact FAT scope depends on the project risk profile, system complexity, regulatory expectations, and agreed qualification strategy.

8. How does MMF support FAT in modular pharma projects?

MMF supports FAT as part of its integrated modular project delivery model. The process connects design, off-site modular construction, equipment integration, factory acceptance testing, transportation, installation, hook-up, validation support, and commissioning. This helps pharmaceutical companies reduce technical uncertainty before shipment and move toward site readiness with greater control.

Designing GMP Cleanrooms for Modular Pharma Facilities

For pharmaceutical manufacturers, cleanroom design is often one of the most critical factors influencing compliance, project timelines, and operational readiness. A cleanroom is not only a controlled space with filtered air. It is an engineered environment where room classification, HVAC performance, pressure cascades, material movement, personnel flow, utilities, cleanroom finishes, monitoring systems, commissioning, and validation must work together.

As pharmaceutical manufacturing moves toward faster, more flexible, and more predictable infrastructure models, modular pharma facilities are becoming a practical approach for new facilities, expansions, and capacity additions. However, the success of any Modular Pharmaceutical Facility depends on how clearly the GMP cleanroom is designed at the beginning of the project.

In modular execution, cleanroom decisions must be finalized early because a large portion of the facility is manufactured, integrated, and checked off-site. When the design is incomplete or unclear, the project may face rework during installation, hook-up, commissioning, or validation. When the design is well defined, modular delivery can support a faster route to GMP readiness with better control over quality and execution.

Why GMP Cleanroom Design Starts With Process Understanding

A GMP cleanroom should always be designed around the manufacturing process. Before deciding the room size, classification, HVAC capacity, or module configuration, the project team must clearly understand the product type, process steps, equipment needs, contamination risks, personnel activities, and material movement.

For example, the cleanroom requirements for sterile filling, vaccine manufacturing, biotech processing, or API handling may differ significantly. Each process has its own expectations for room classification, air change rates, pressure relationships, containment, utility demand, cleaning approach, and environmental monitoring.

This is why early-stage Design & Engineering becomes important in a modular facility project. A well-developed design helps define the cleanroom zones, equipment placement, service corridors, utility routes, pass boxes, airlocks, gowning areas, and future expansion possibilities before the modules move into manufacturing.

When process requirements are clearly translated into engineering design, the modular facility becomes easier to manufacture, transport, install, qualify, and operate.

Cleanroom Classification and GMP Zoning

Cleanroom classification is one of the first technical decisions in GMP facility design. The required classification depends on the product exposure level, manufacturing operation, contamination risk, and applicable regulatory expectations.

In pharmaceutical manufacturing, cleanrooms are typically planned using controlled zones such as Grade A, B, C, and D or ISO-based classifications, depending on the process and regulatory framework. The objective is to provide the right level of environmental control without overdesigning the facility.

For modular cleanrooms, zoning must be integrated into the module layout from the start. Critical areas should be protected with appropriate airlocks, pressure cascades, HEPA filtration, and controlled access. Lower-grade areas should support material preparation, equipment movement, gowning, and support activities without compromising higher-grade zones.

Good zoning also helps optimize CAPEX and OPEX. Instead of treating the entire facility as one highly classified area, the cleanroom can be engineered with appropriate classification levels based on actual process risk. This supports compact, efficient, and GMP-aligned pharmaceutical facility design.

Personnel Flow and Material Flow in Modular Cleanrooms

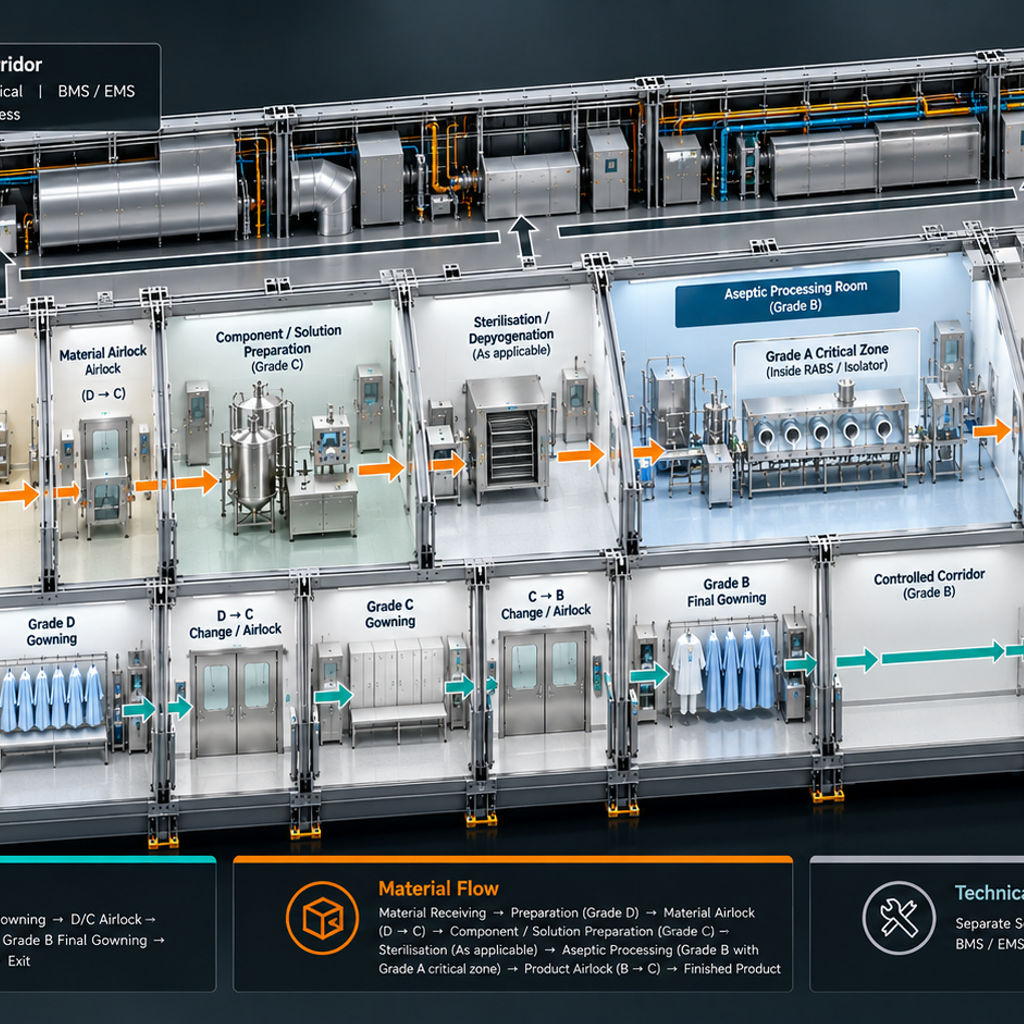
A cleanroom layout should reduce unnecessary movement and prevent cross-contamination. Personnel flow and material flow must be clearly separated wherever required, especially in facilities handling sterile products, biologics, vaccines, or sensitive pharmaceutical processes.

Personnel movement typically includes entry, gowning, transition through airlocks, process area access, and exit flow. Material movement may include raw materials, components, consumables, equipment parts, packaging materials, waste, and finished goods. If these flows are not properly planned, the risk of contamination, mix-ups, pressure disturbance, and operational inefficiency increases.

In a modular pharma facility, these flows also influence module interfaces. Door positions, pass-through systems, interlocking arrangements, airlocks, corridor widths, and transfer routes need to be coordinated during the design stage. Any late change after module fabrication can affect structural design, HVAC balancing, utility routing, and validation documentation.

MMF’s approach connects workflow planning with Off-site Modular Construction, allowing cleanroom layouts and critical interfaces to be developed in a controlled factory environment before site installation. 

HVAC, HEPA Filtration, and Pressure Cascades

HVAC is one of the most critical systems in GMP cleanroom engineering. It controls temperature, humidity, air cleanliness, airflow direction, pressure differentials, and particle control. In pharmaceutical manufacturing, HVAC is not only a comfort system; it is a product protection system.

A well-designed cleanroom HVAC system should consider:

  • Air change requirements
  • HEPA filtration
  • Airflow patterns
  • Room pressure relationships
  • Temperature and humidity control
  • Return air strategy
  • Fresh air requirements
  • Exhaust needs
  • Equipment heat load
  • Operator movement
  • Monitoring points
  • Utility integration

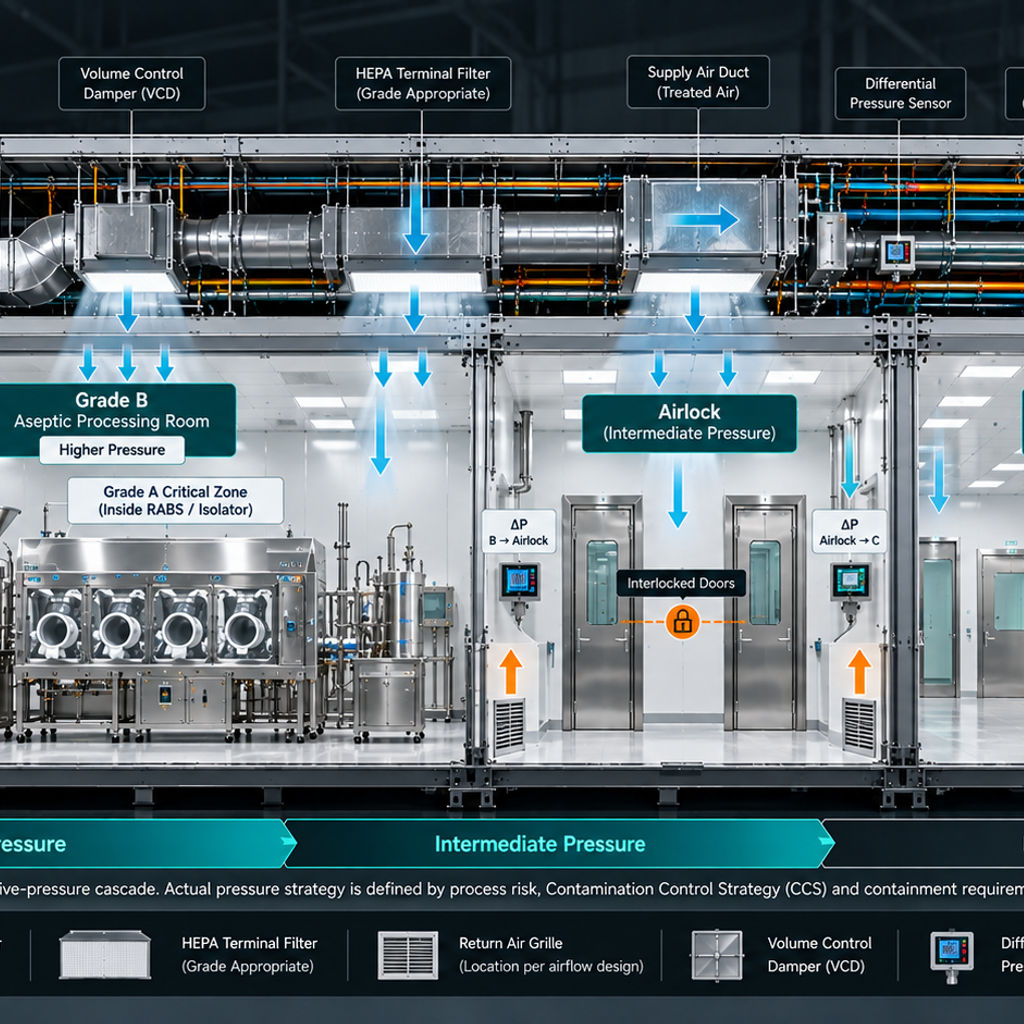
Pressure cascades help maintain airflow from cleaner areas toward less clean areas. This is especially important in sterile or high-control environments where exposed product, components, or critical process steps must be protected. In some applications, negative pressure or containment logic may be required depending on product risk.

For Modular Cleanrooms, HVAC routing must be coordinated with the module structure, ceiling height, utility zones, service access, and transportation limits. Ducting, terminal filters, dampers, sensors, and control systems should be planned before off-site fabrication begins.

By integrating HVAC, electrical systems, EMS, BMS, utilities, and cleanroom envelope requirements during manufacturing, MMF supports a more controlled and predictable execution pathway.

Cleanroom Finishes and Modular Envelope Design

The cleanroom envelope plays an important role in GMP compliance. Walls, ceilings, flooring, doors, windows, joints, coving, and service penetrations should support cleaning, disinfection, durability, and contamination control.

Cleanroom finishes should generally be smooth, non-shedding, easy to clean, resistant to cleaning agents, and suitable for the intended manufacturing environment. Poor detailing around joints, panels, service penetrations, or ceiling interfaces can create cleaning challenges and long-term maintenance risks.

In modular cleanroom construction, much of the cleanroom envelope is manufactured in a controlled environment. This allows better coordination between structural framing, wall panels, flooring, HVAC openings, utilities, lighting, and access points. It also reduces dependency on extensive site-based finishing work.

This controlled off-site approach supports consistency and reduces the risk of variation that can occur when multiple construction activities are handled sequentially at site.

Utility Integration in GMP Cleanroom Design

A GMP Manufacturing Facility requires more than cleanroom panels and HVAC. Process utilities and clean utilities must be planned in coordination with equipment requirements and cleanroom operations.

Depending on the process, utility integration may include purified water, WFI, clean steam, compressed air, nitrogen, process gases, chilled water, hot water, vacuum, drainage, electrical distribution, automation, EMS, and BMS systems.

In modular pharma facilities, utility planning is especially important because many utility routes, service connections, and equipment interfaces are pre-integrated before shipment. This requires accurate load calculations, space planning, maintenance access, connection points, and hook-up strategy.

Early utility coordination supports smoother Installation & Hook-up and reduces delays during commissioning. It also helps the project team avoid clashes between cleanroom layout, equipment arrangement, HVAC routing, and process utility distribution.

Factory Acceptance Testing for Modular Cleanrooms

One of the major advantages of modular execution is the ability to complete key checks before the facility reaches the site. Factory Acceptance Testing allows project teams to verify selected systems, components, interfaces, and documentation during or after off-site manufacturing.

For GMP cleanrooms, FAT may include checks related to module construction, equipment installation, utility integration, HVAC components, electrical systems, automation panels, documentation readiness, and functional performance depending on the project scope.

This does not replace site qualification or validation. However, it helps identify and resolve issues earlier, before transportation and installation. For pharmaceutical project teams, early testing can reduce site uncertainty, support faster commissioning, and improve confidence before final qualification activities begin.

MMF’s approach places strong importance on FAT because modular facilities are designed, manufactured, integrated, and checked before being shipped to the final project site.

Commissioning and Validation Support

Cleanroom performance must be demonstrated through proper commissioning, qualification, and validation activities. A modular facility still requires documented evidence that the cleanroom, utilities, equipment, and systems are installed correctly and operate as intended.

Validation planning should begin during the design stage. This helps align the User Requirement Specification, design qualification, installation qualification, operational qualification, performance qualification, FAT documentation, commissioning records, and final handover package.

For modular GMP facilities, validation boundaries must be clearly defined. The project team should identify what is tested at the manufacturing facility, what is verified after transportation, what is checked during hook-up, and what must be qualified at the final site.

MMF supports this lifecycle approach through Validation & Commissioning, helping pharmaceutical companies move from modular manufacturing to operational readiness with better documentation control and project clarity.

Why Modular Cleanroom Design Supports Faster Facility Delivery

Traditional pharmaceutical facility construction can be affected by site dependency, sequential activities, coordination delays, weather exposure, local labour limitations, and late-stage design changes. Modular cleanroom delivery addresses many of these challenges by shifting a large part of construction, integration, and checking into a controlled off-site environment.

This approach allows site preparation and module manufacturing to progress in parallel. It also supports better coordination between engineering, cleanroom envelope, HVAC, utilities, equipment placement, and documentation.

For pharmaceutical manufacturers, biotechnology companies, CDMOs, vaccine manufacturers, and facility owners, this can support faster project delivery without compromising the engineering discipline required for GMP compliance.

However, the value of modular construction depends on strong front-end design. If process requirements, cleanroom classification, utility loads, equipment interfaces, and validation expectations are not clearly defined early, modular execution can face the same delays as conventional construction.

Why Choose Modular Mobile Facility (MMF)?

Modular Mobile Facility (MMF) helps pharmaceutical companies plan and execute GMP-ready modular infrastructure through an integrated project delivery model. From Design & Engineering and Off-site Modular Construction to Manufacturing, Factory Acceptance Testing, Transportation, Installation & Hook-up, and Validation & Commissioning, MMF brings key stages of facility delivery into one coordinated pathway.

For companies planning a new Modular Pharmaceutical Facility, facility expansion, cleanroom addition, or faster route to GMP manufacturing readiness, MMF provides engineering-led modular solutions designed for compliance, predictable execution, and scalable pharmaceutical manufacturing.

Frequently Asked Questions 

1. What is GMP cleanroom design for modular pharma facilities?

GMP cleanroom design for modular pharma facilities involves planning controlled environments that support pharmaceutical manufacturing, contamination control, HVAC performance, pressure cascades, personnel flow, material flow, utilities, and validation requirements. In modular execution, these cleanroom systems are designed and integrated before off-site manufacturing begins, allowing the facility to be built, checked, transported, installed, and commissioned with better project control.

2. Can modular cleanrooms meet GMP requirements?

Yes, modular cleanrooms can meet GMP requirements when they are properly designed, engineered, manufactured, installed, qualified, and validated. The construction method does not define compliance by itself. Compliance depends on cleanroom classification, HVAC design, pressure control, cleanable finishes, workflow segregation, documentation, monitoring systems, and validation evidence.

3. Why is HVAC important in a GMP cleanroom?

HVAC is critical because it controls air cleanliness, airflow direction, temperature, humidity, pressure differentials, and contamination protection. In pharmaceutical cleanrooms, HVAC directly supports product quality and regulatory compliance. Poor HVAC planning can affect pressure cascades, particle control, operator comfort, equipment performance, and cleanroom qualification.

4. What are pressure cascades in pharmaceutical cleanrooms?

Pressure cascades are controlled pressure relationships between rooms of different cleanliness levels. They help ensure that air moves from cleaner areas toward less clean areas, reducing contamination risk. In modular cleanrooms, pressure cascades must be planned early because they affect HVAC design, airlocks, door interlocks, room layout, monitoring points, and commissioning activities.

5. Why is Factory Acceptance Testing important in modular cleanroom projects?

Factory Acceptance Testing helps verify selected systems, components, and interfaces before the modular facility is shipped to site. For modular cleanrooms, FAT can help identify issues earlier, reduce installation errors, support documentation readiness, and shorten the path to commissioning. It is especially useful when HVAC, utilities, equipment, electrical systems, and automation are pre-integrated off-site.

6. When should validation planning begin for a modular pharma facility?

Validation planning should begin during the design stage. Early planning helps align URS, design qualification, FAT scope, installation qualification, operational qualification, performance qualification, and final handover documentation. In modular projects, this is important because some checks may happen at the manufacturing facility, while others must be completed after transportation, installation, and hook-up.

7. What are the main design factors for modular cleanrooms?

The main design factors include cleanroom classification, process flow, personnel flow, material flow, HVAC design, HEPA filtration, pressure cascades, cleanroom finishes, equipment layout, utility integration, automation, monitoring systems, maintenance access, FAT requirements, commissioning strategy, and validation planning.

8. How does modular construction help pharmaceutical facility delivery?

Modular construction helps pharmaceutical facility delivery by allowing a large portion of construction, integration, and testing to happen in a controlled off-site environment. This can reduce site dependency, improve coordination, support parallel execution, and create a more predictable route from design to installation, hook-up, commissioning, and validation.